The proof exists. Putting your hand on it is the problem.
Your test results, sign-offs and photos already exist. They’re spread across cabinets, folders and phones. CONQA is construction QA software built on proof: it records each one at the board as it’s built, so when a board is questioned months after dispatch, you answer from the record in seconds, on your phone or in the office.
What happened with this board? Bang, look up the project number, and it’s there. It’s instant.– Trevor Cooper, QA Manager, Border Switchboards
Recorded at the board, as it’s built.
On paper, the proof lives in cabinets of boards and folders of photos someone attached by hand. In a rush week, ten boards out the door, the paperwork runs weeks behind the dispatch. When a client calls about a board, someone goes digging.
CONQA records the check where the work happens, against the board itself. Some of the evidence physically disappears as the board is built: bus bar work gets enclosed, and once it’s sealed you can’t get to it again. So the section is photographed and signed off before it closes, and the board’s record stays open until the last section is done.
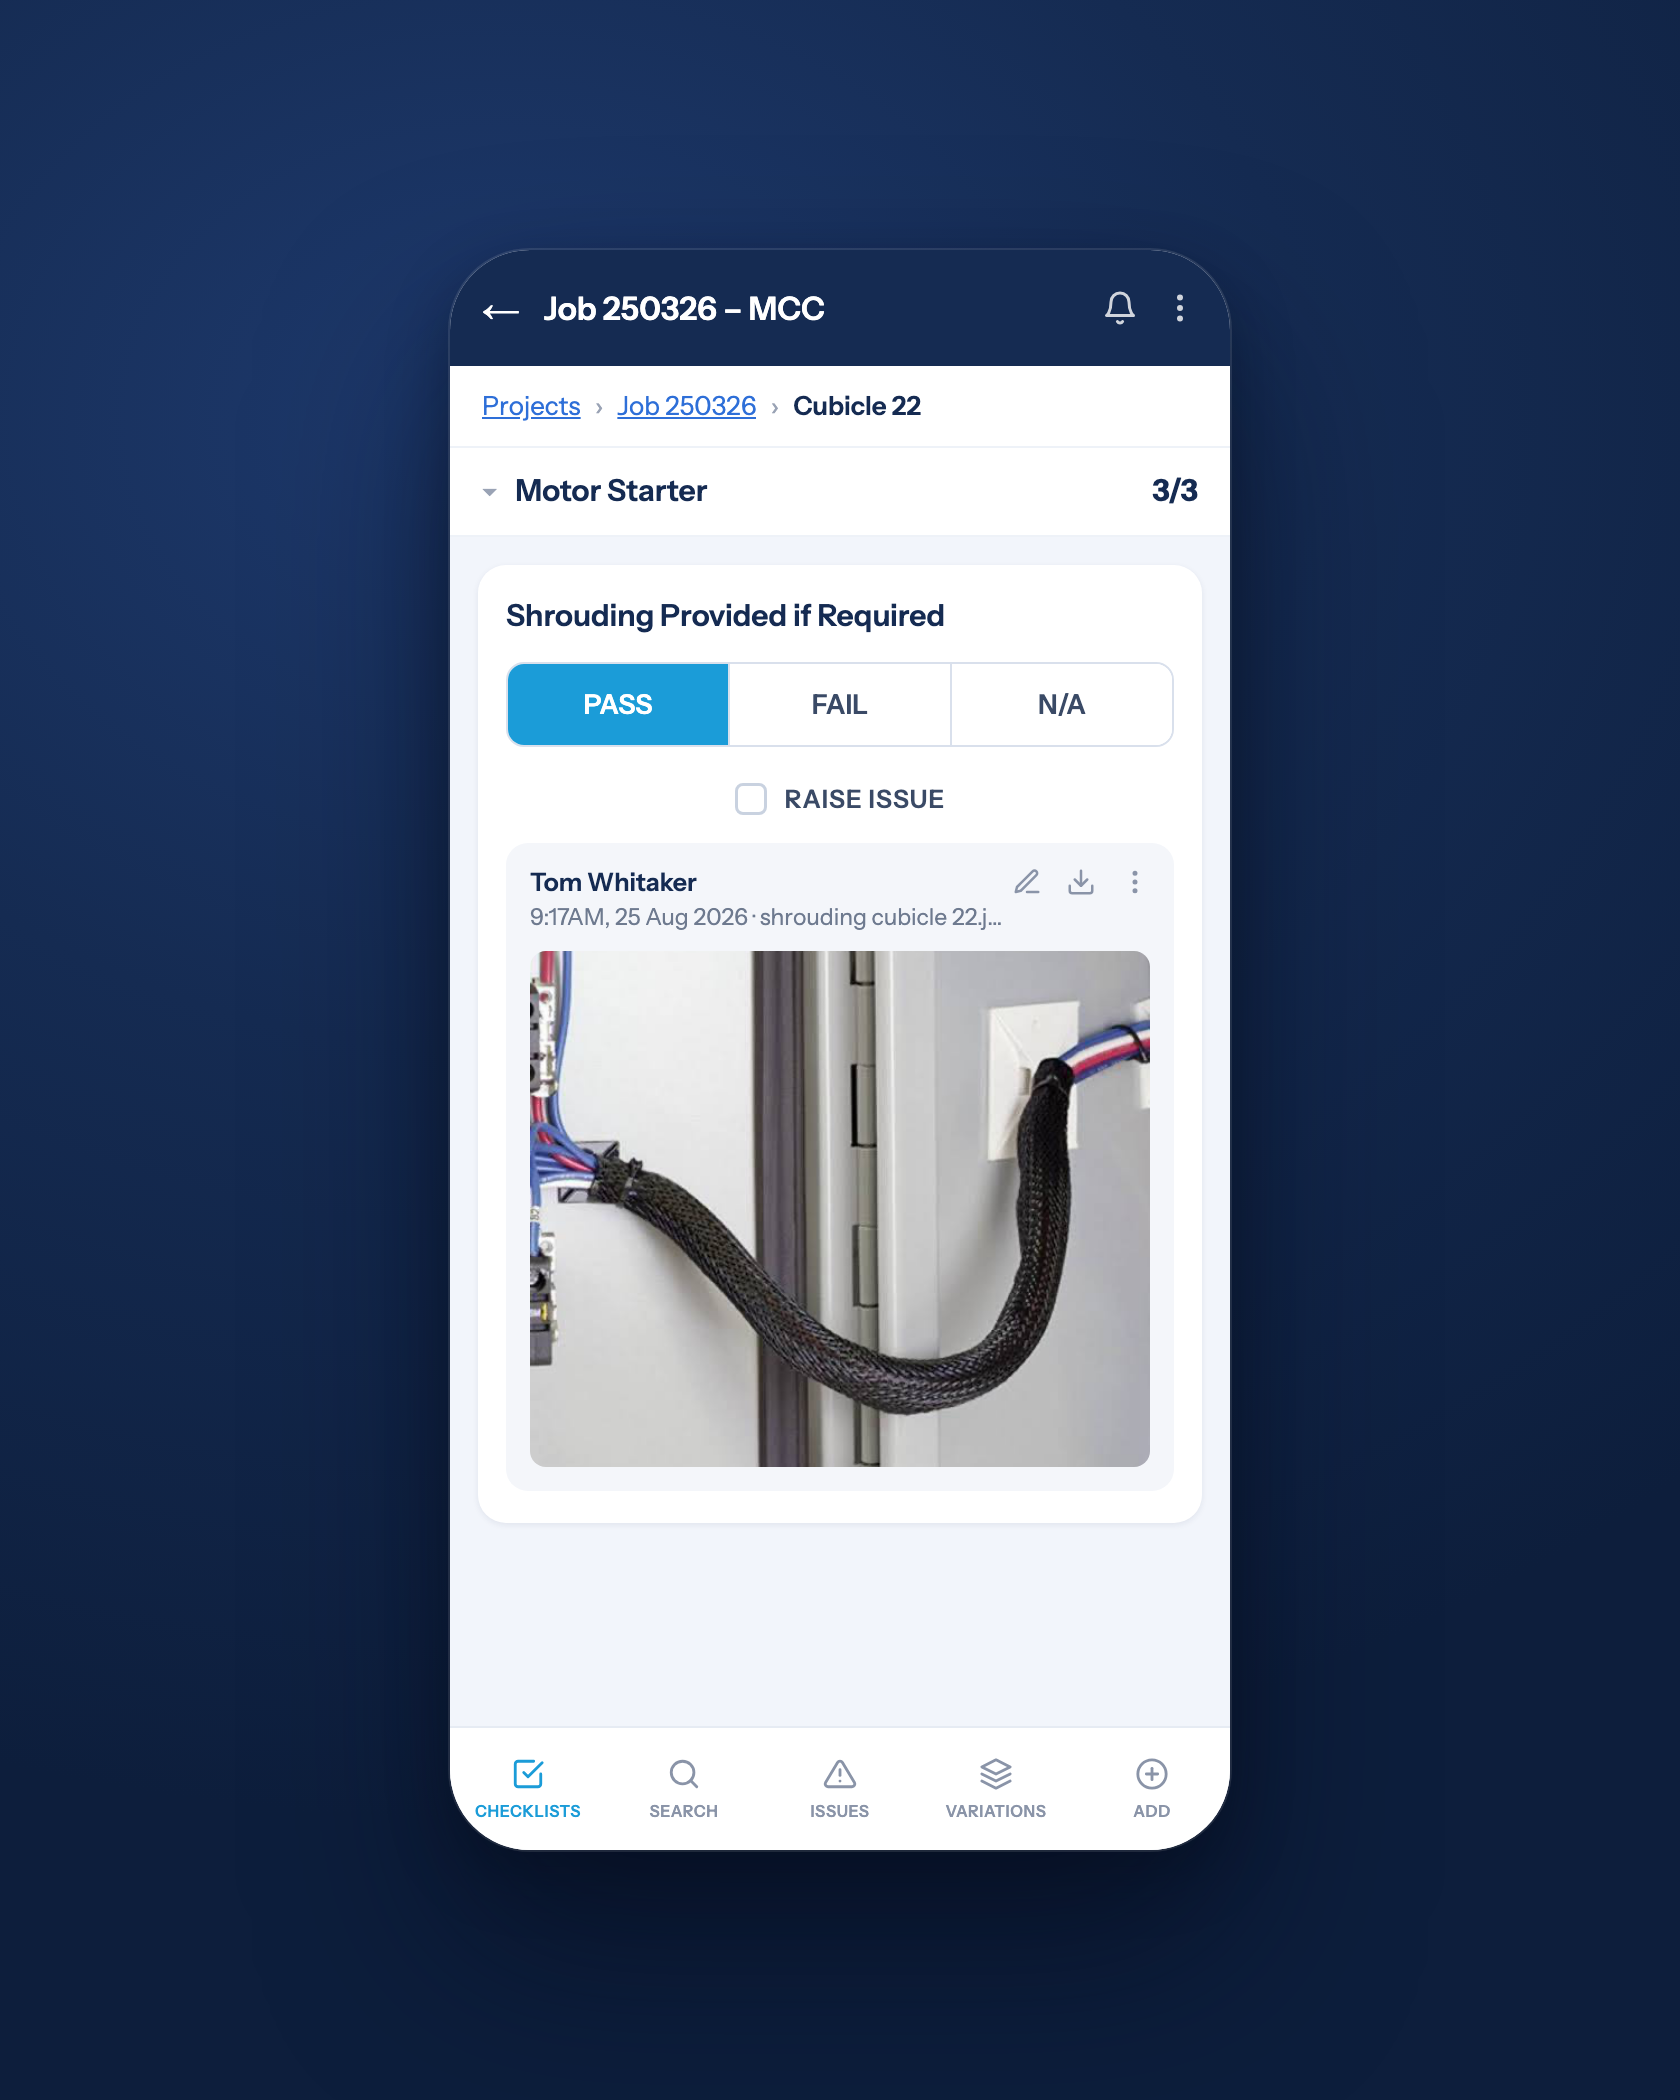
Captured at the board, filed against the unit. Sections photographed before they’re enclosed.
The question comes back six months after the board leaves.
“Was this a faulty product? And it’s like, well, no. Here’s the proof that it was fine.”
a QA manager at a switchboard manufacturer
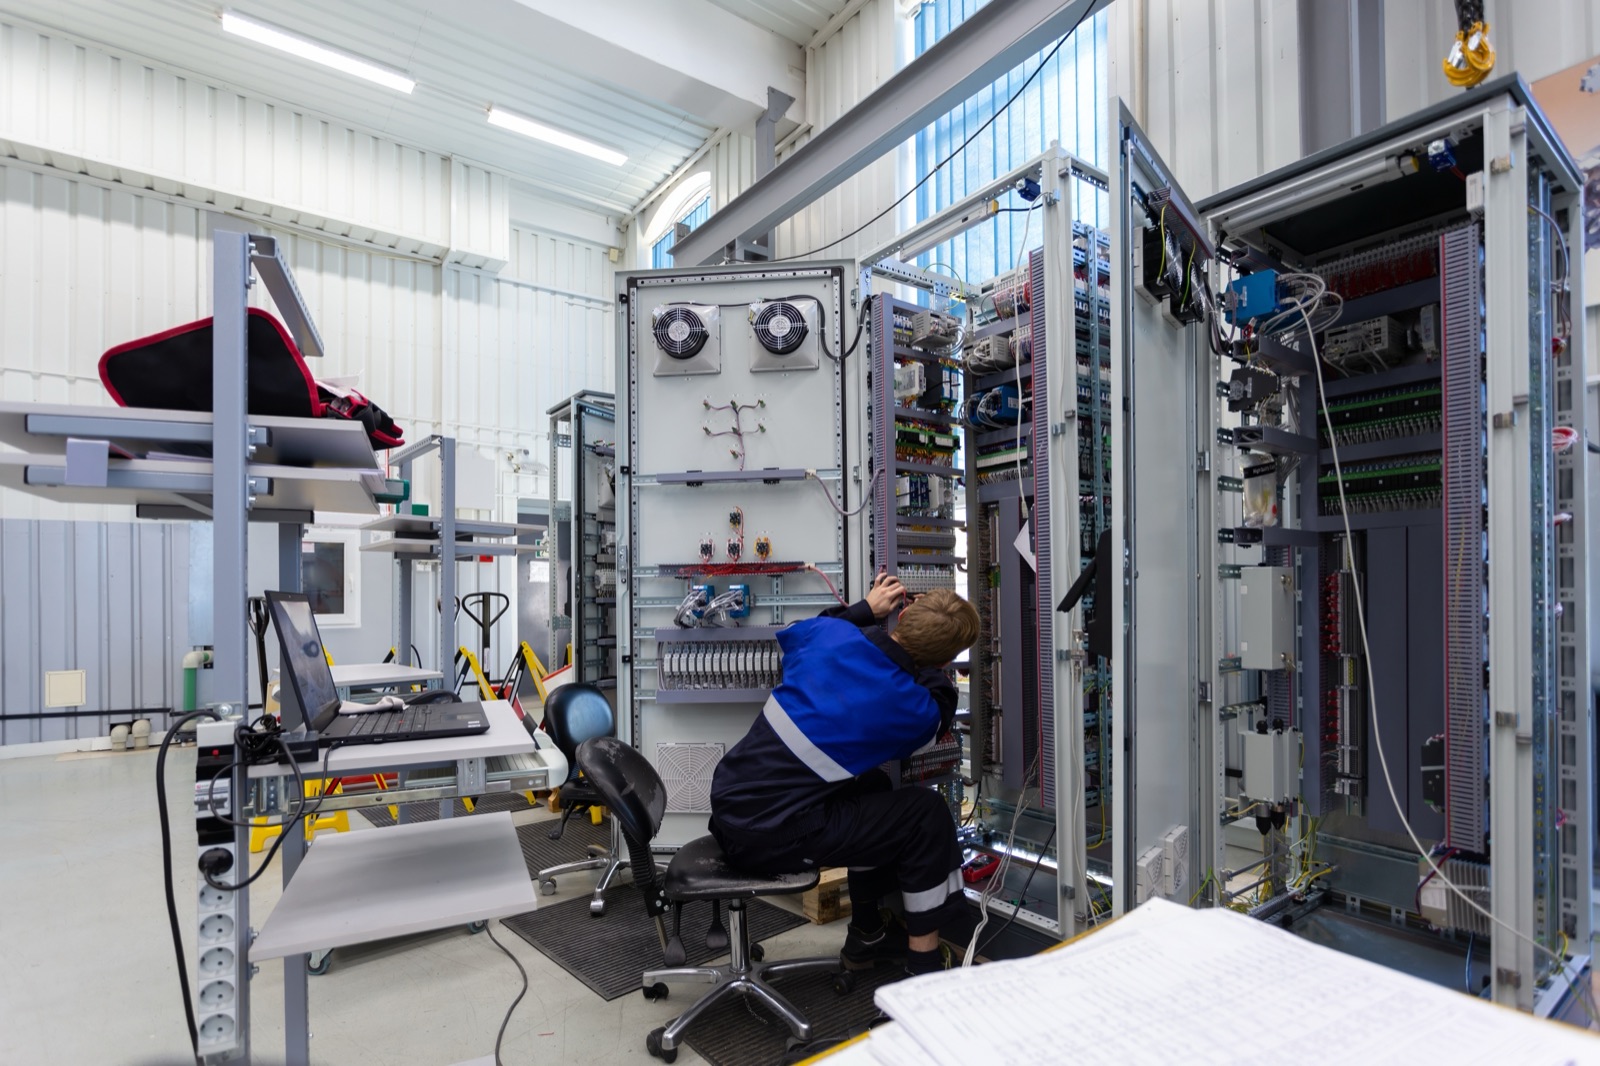
“This is how it left us” only counts if you can prove it.
When a board is questioned in the field (a failed test, damage blamed on the factory, a fault that could have come from transit or install), the cost defaults to the maker unless the record says otherwise. The work was right when it left you. What decides the dispute is whether you can show it: what was built, what was tested, who signed it off, and what it looked like the day it shipped.
CONQA builds that record as the board moves through the shop, tied to the unit itself. When the phone call comes, months later, you answer from the record, not from memory. One switchboard manufacturer answered a disputed megger test that way, with the test records pulled up on a phone. A cable claimed as factory damage was answered from the dispatch photos. A board questioned after a long road trip was settled by the bus-resistance reading taken before it left.
“when it left us, this is what it looked like”
– Trevor Cooper, QA Manager, Border Switchboards
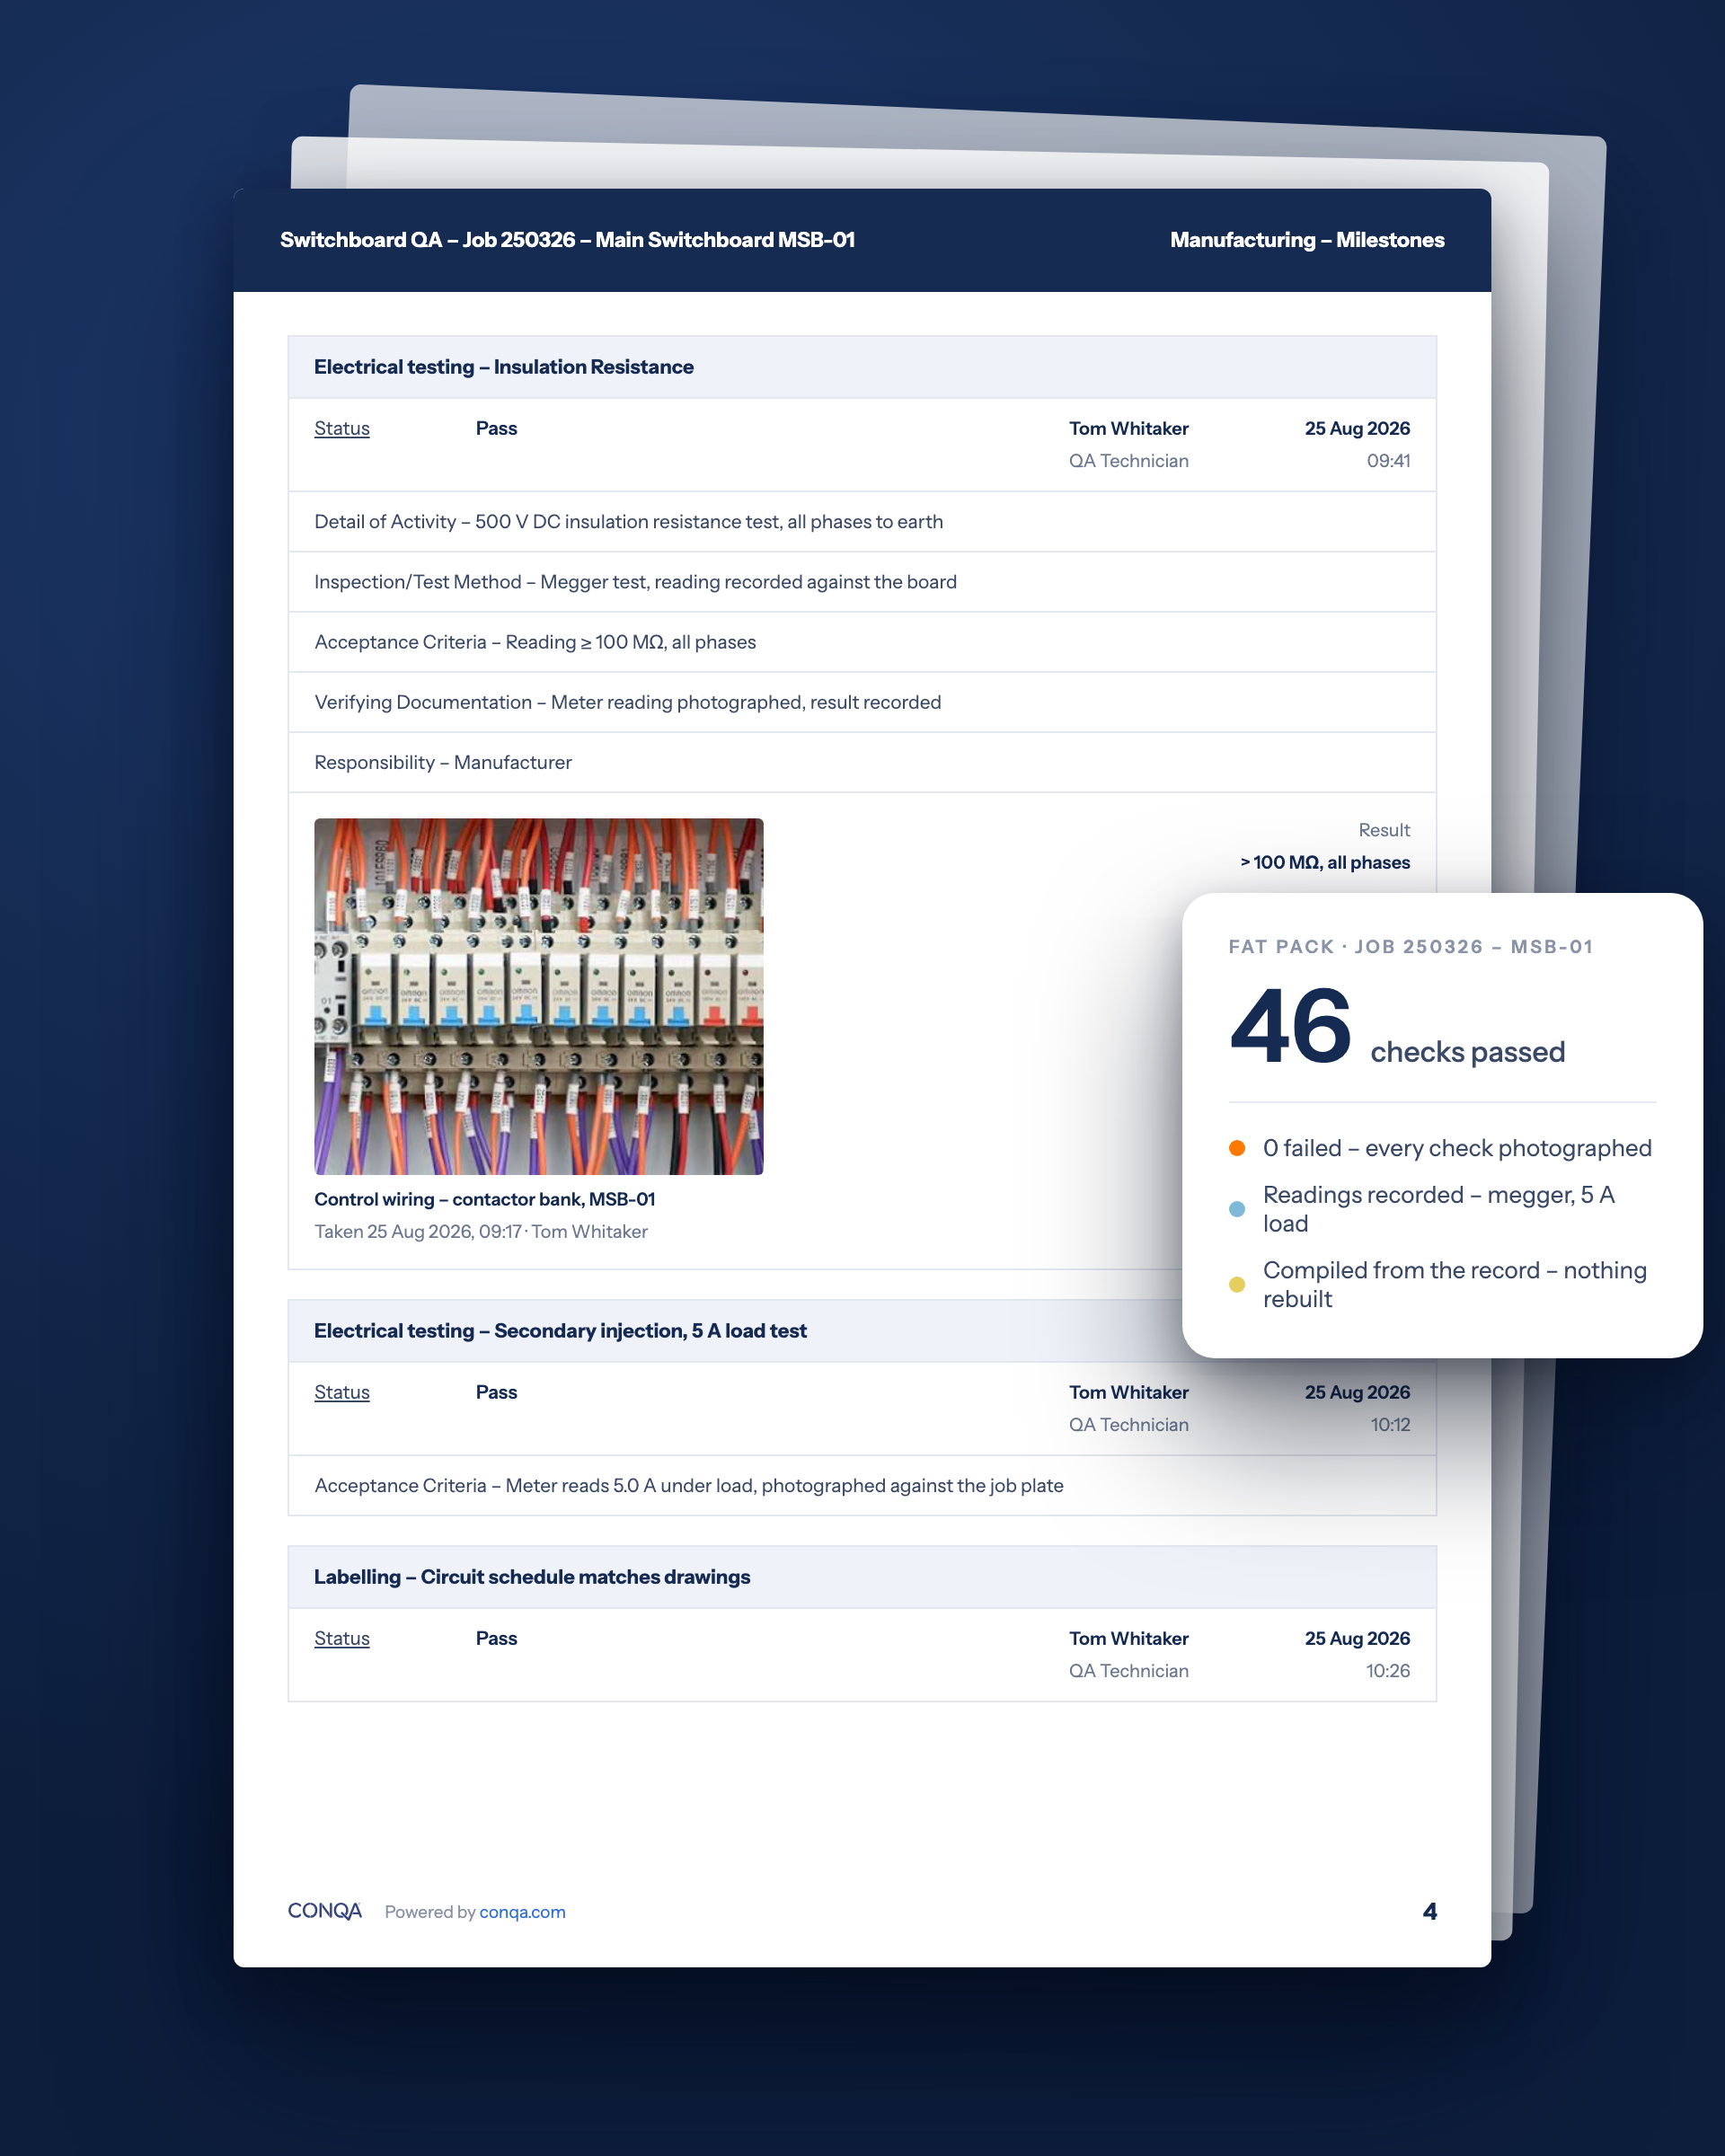
Every check, test result and sign-off, in the board’s own record.
FAT is your QA on show. The record is what makes it credible.
Factory acceptance testing is the one moment the client stands in your workshop and judges how you work. A board backed by a complete record answers the question before it’s asked: every check signed, every test result recorded, “a photo taken of the meter reading five amps, so you can prove the stuff was working when it left the factory”. A board backed by loose paper and a folder of photos raises it, however good the work is.
One motor control centre had thirty-odd cubicles, each with its own checklist and test record. A visiting consultant went through the pack and compared it with what competitors hand over. In Trevor Cooper’s words: “Everyone’s seen reports that just say tick, tick, tick, tick. Whereas this is a detailed document saying passed, this time, by who, with photo evidence that backs up that information.” The same record that defends the board after dispatch is the one that carries the FAT, the handover pack, and the next tender.
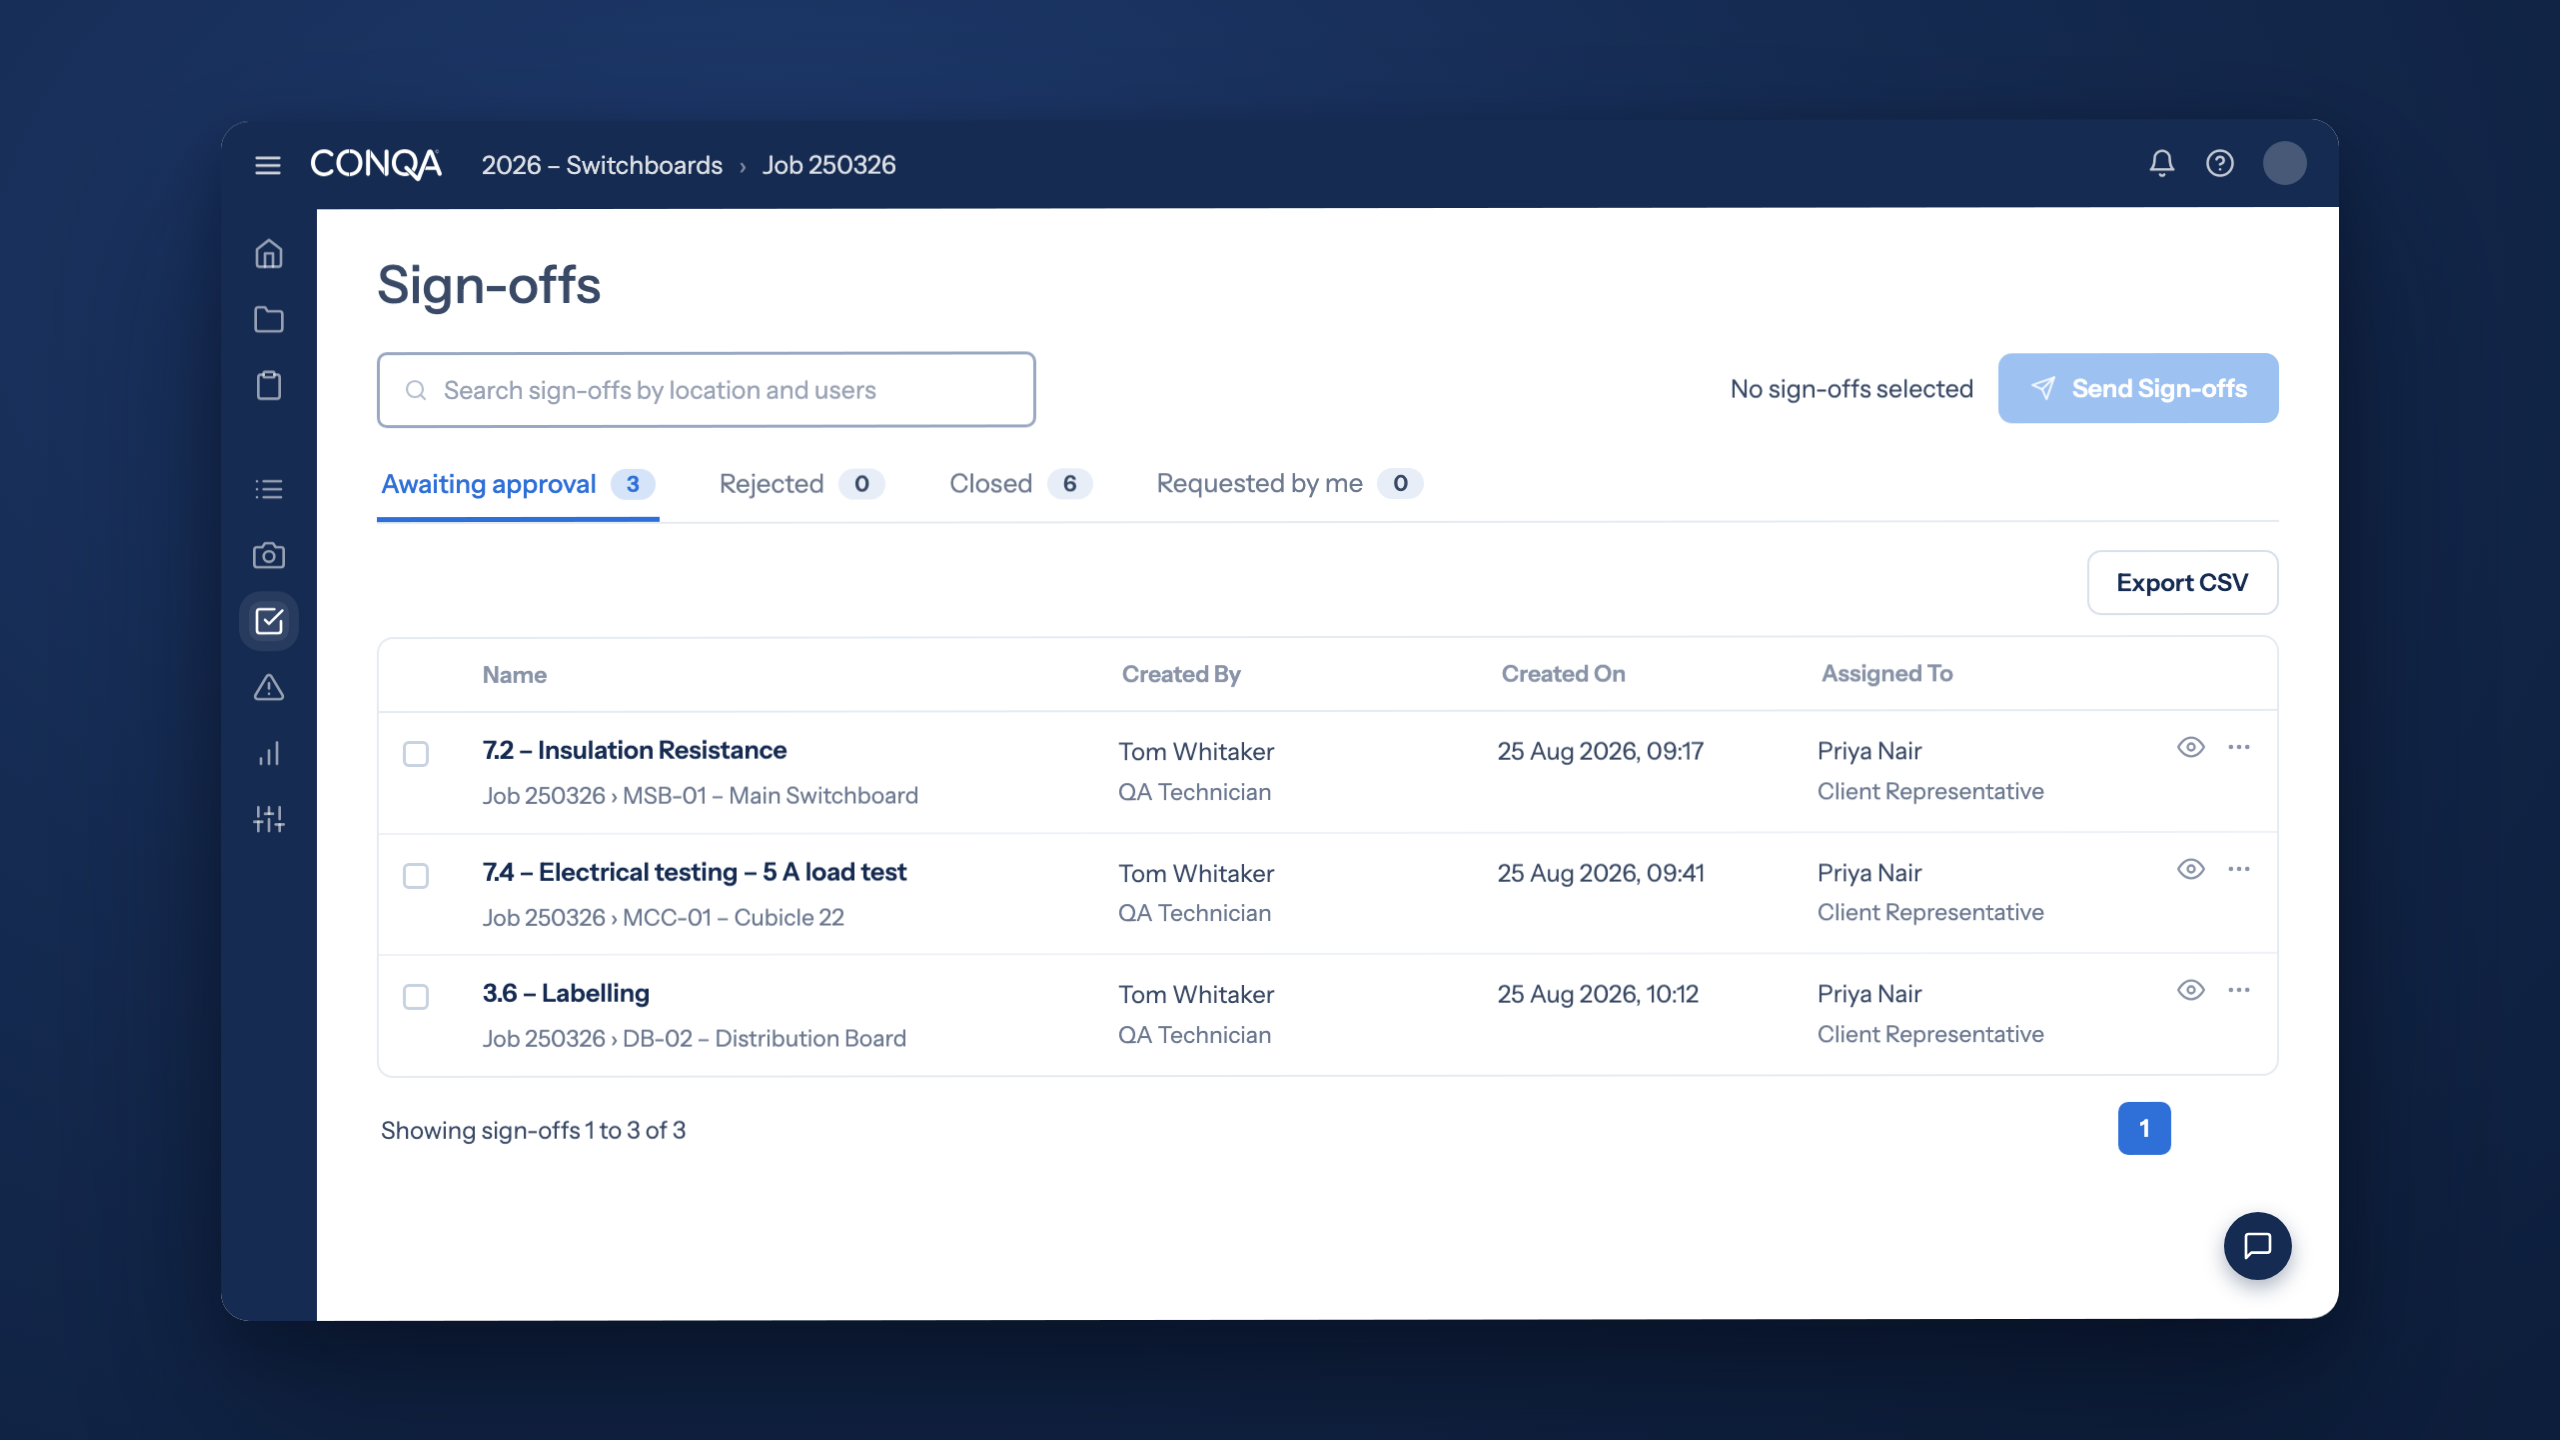
The record behind the test, ready to show the day the client walks the floor.
What switchboard manufacturers told us.
“You can reference back to the very first one and they can be built exactly the same, rather than ‘pretty sure this is what we did.’”
– Trevor Cooper, QA Manager, Border Switchboards“One good catch with a good system could save us a huge amount of money.”
– a QA lead at a switchboard manufacturer“I can’t see why they would change.”
– a switchboard manufacturerCommon questions
What does CONQA do for switchboard manufacturers?
CONQA is construction quality assurance software built on proof. Tests and sign-offs are captured as the board is built and filed against the unit itself, so every board leaves the factory with its own record of what was built, what was tested, who signed it off and what it looked like at dispatch. That record answers for the board if it is ever questioned.
Can CONQA help with a disputed board after dispatch?
The record shows the state the board left the factory in: test results, sign-offs and photos, dated before dispatch. One switchboard manufacturer rebutted a megger-test dispute straight from the record, from a phone, and answered a damaged-in-transit cable claim the same way. Without the record, the cost of a disputed board defaults to the maker.
How does CONQA support factory acceptance testing?
The record behind the FAT is built as the board moves through the shop, so there is nothing to assemble when the client arrives. They walk the board with a printed or emailed report showing every check signed and every test result: readings and photos, not pages of ticks. The same record carries the handover pack and the next tender.
Can CONQA handle complex boards like MCCs?
Yes. Each cubicle on a motor control centre carries its own checklist and test record. On a thirty-cubicle MCC, that is thirty individual records. When one motor is questioned, you produce that cubicle’s tests, photos and sign-offs, not a single report for the whole board.
Does CONQA replace our ERP or production systems?
No. CONQA is the independent QA record. It runs alongside your ERP, scheduling system and spreadsheets rather than replacing them. The record is exportable in full and yours to keep.
What does implementing CONQA involve?
There is no migration: the record starts on the next board, not with the backlog. And there is no integration: boards are added one at a time as they reach QA, which is how the switchboard manufacturers we work with choose to run it. A generic board checklist works from day one, and your own team adds board-specific templates as they need them. One manufacturer moved straight off paper. A year later, his verdict was “I can’t see why they would change.”
We’re flat out. Is now the right time?
A rush week is exactly when paper falls behind. One manufacturer described boards shipping three weeks ahead of their paperwork. Every board that leaves without a record is unprotected for the length of its liability window. Starting doesn’t interrupt production: the next board gets checked in CONQA instead of on paper, and the ones after it follow.
How much does CONQA cost?
CONQA starts at $899 a month for manufacturers. Pricing scales with the size of your operation. There’s no per-user charge, so everyone who needs to see the record gets access. Book a demo and we’ll give you a firm number for your workshop.
No migration, no integration. The record starts on the next board that reaches QA.
The board leaves. The proof leaves with it.
See the record a board carries out of the workshop.