“This is how it left us” only counts if you can prove it.
CONQA is construction quality assurance software built on proof: the record that shows every board was right when it left you. A switchboard goes into someone else’s plant room, someone else’s install, someone else’s story about why it failed. The record is what keeps their story from becoming your cost.
A disputed board is yours to own – unless the record was already there.
When a board is questioned in the field – a failed test, damage blamed on the factory, a fault that could have come from transit or install – the cost defaults to the maker unless the record says otherwise. The work was right when it left you. Everyone in your workshop knows it. What decides the dispute is whether you can show it: what was built, what was tested, who signed it off, and what it looked like the day it shipped.
CONQA builds that record as the board moves through the shop, tied to the unit itself. When the phone call comes, months later, you answer from the record, not from memory. One switchboard manufacturer rebutted a megger-test dispute that way – the QA manager pulled the test records up on his phone, on holiday, and traced the fault to the install. A damaged-in-transit cable claim was answered from the dispatch photos, and a board questioned after crossing Western Australia by road was settled by the bus-resistance reading recorded at dispatch: 100 micro-ohms, end to end.
“when it left us, this is what it looked like”
– a switchboard manufacturer
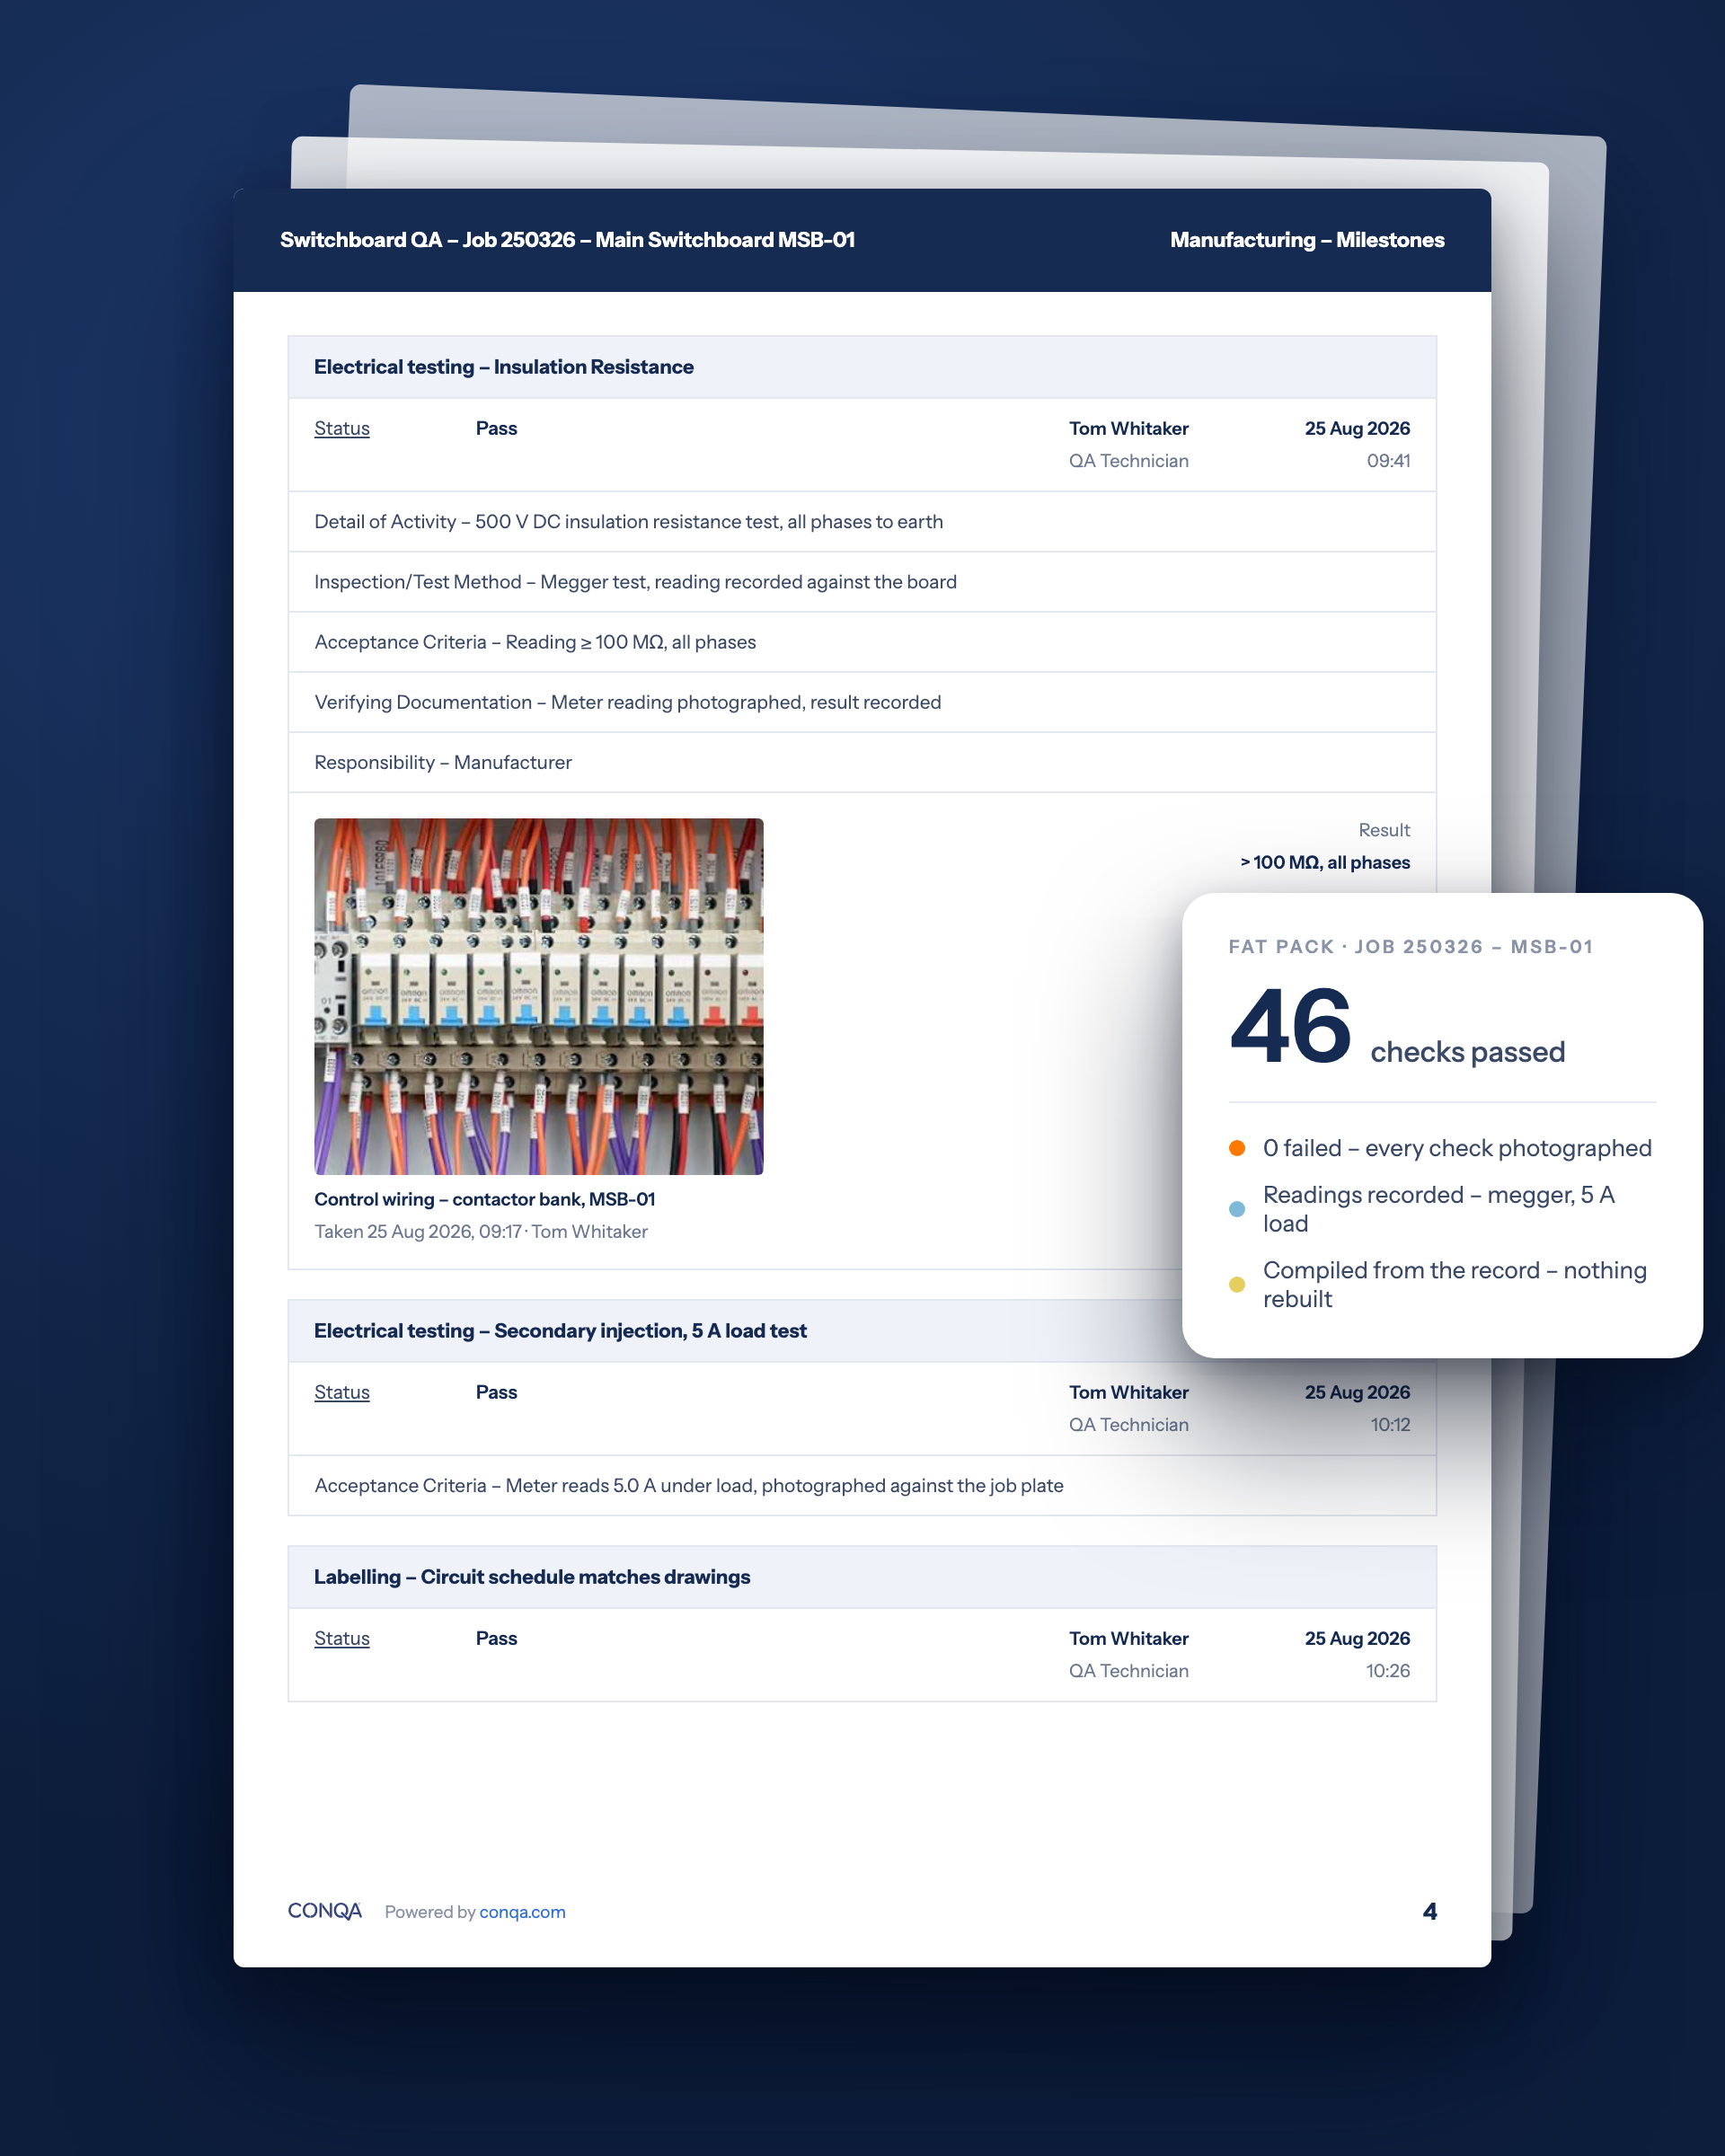
Every check, test result and sign-off filed against the unit.
The question comes back six months after the board leaves.
“Was this a faulty product? And it’s like, well, no, because here’s the proof that it was fine.”
a switchboard manufacturer
The proof exists. Putting your hand on it is the problem.
On paper, the proof lives in cabinets of boards and folders of photos someone attached by hand. In a rush week – ten boards out the door – the paperwork runs weeks behind the dispatch, and when a client calls about a board, someone goes digging.
CONQA records the check where the work happens, against the board itself. Some of the evidence physically disappears as the board is built: bus bar work gets enclosed, and once it’s sealed you can’t get to it again. So the section is photographed and signed off before it closes, and the board’s record stays open until the last section is done. Nothing is assembled afterwards, because there’s nothing to assemble.
Months or years later, the question takes seconds, from anywhere – the record is the same on a phone as it is in the office.
“What happened with this board? Bang, look up the project number, and it’s there. It’s instant.”
– a switchboard manufacturer
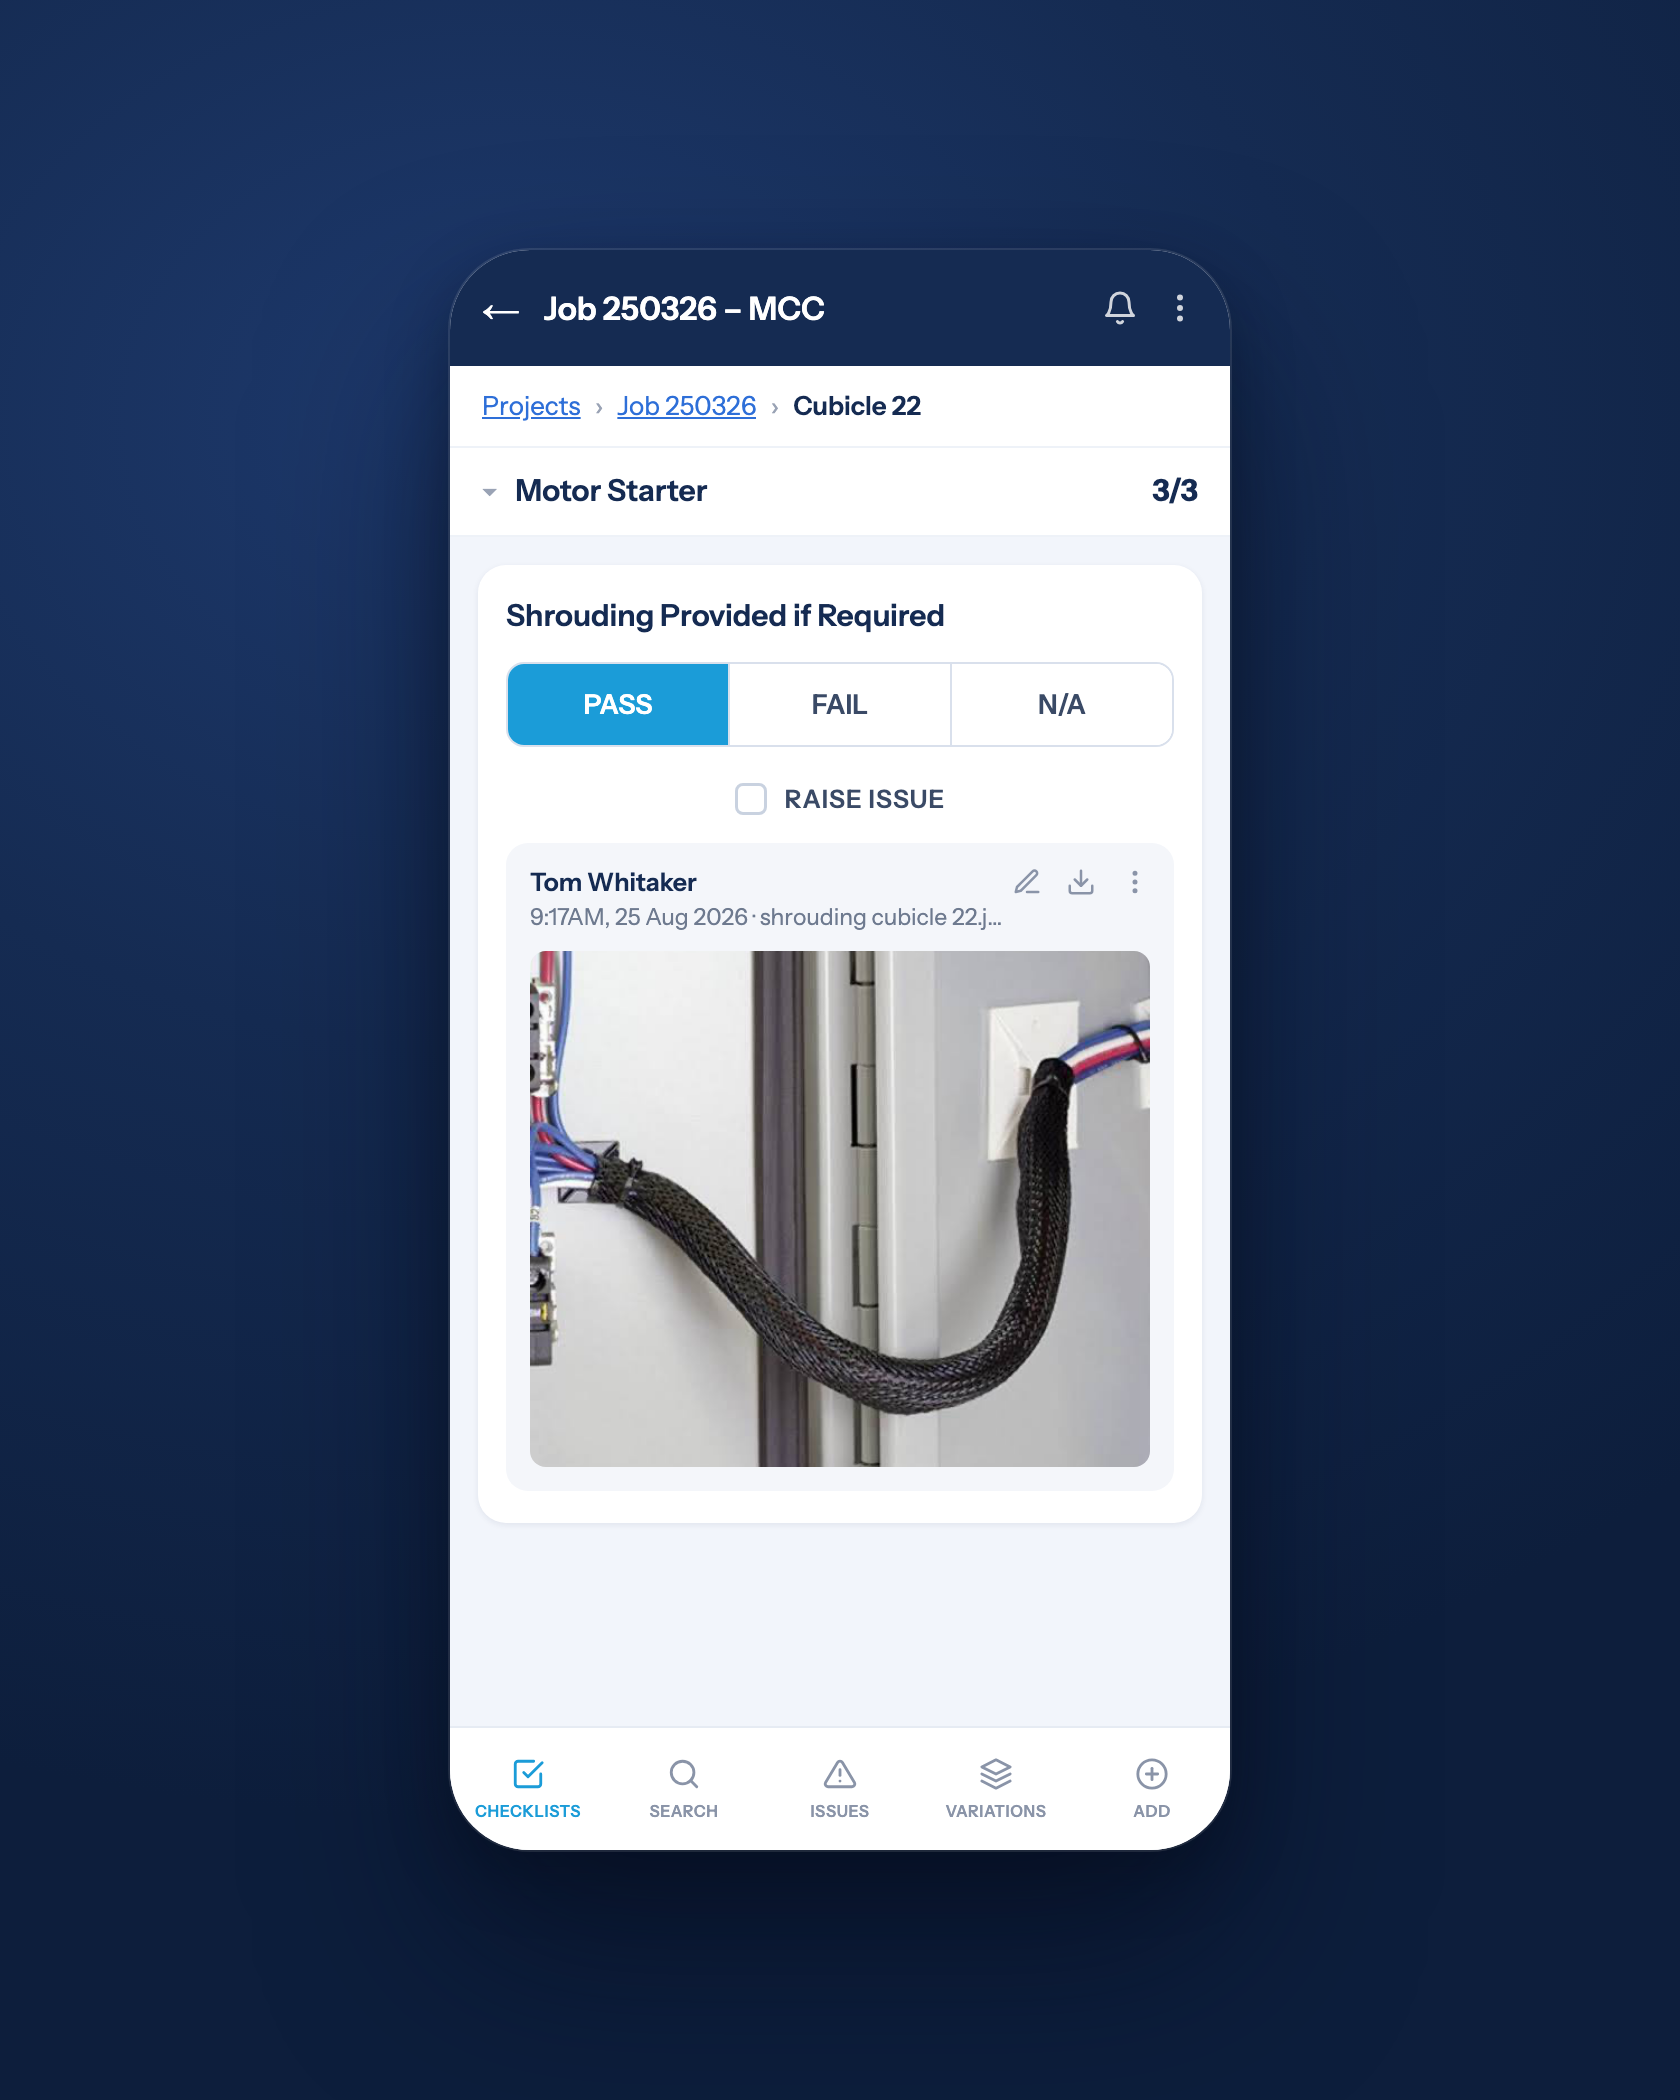
Captured at the board, filed against the unit. Sections photographed before they’re enclosed.
FAT is your QA on show. The record is what makes it credible.
Factory acceptance testing is the one moment the client stands in your workshop and judges how you work. A board backed by a complete record – every check signed, every test result filed against the unit, the meter photographed at five amps under load – answers the question before it’s asked. A board backed by loose paper and a folder of photos raises it, however good the work is.
On one motor control centre – thirty-odd cubicles, each with its own checklist and test record – a visiting consultant compared the pack against what competitors hand over: pages of ticks on one side; on the other, each cubicle’s tests marked passed, dated, signed, with the photos behind them. The same record that defends the board after dispatch is the one that carries the FAT, the handover pack, and the next tender.
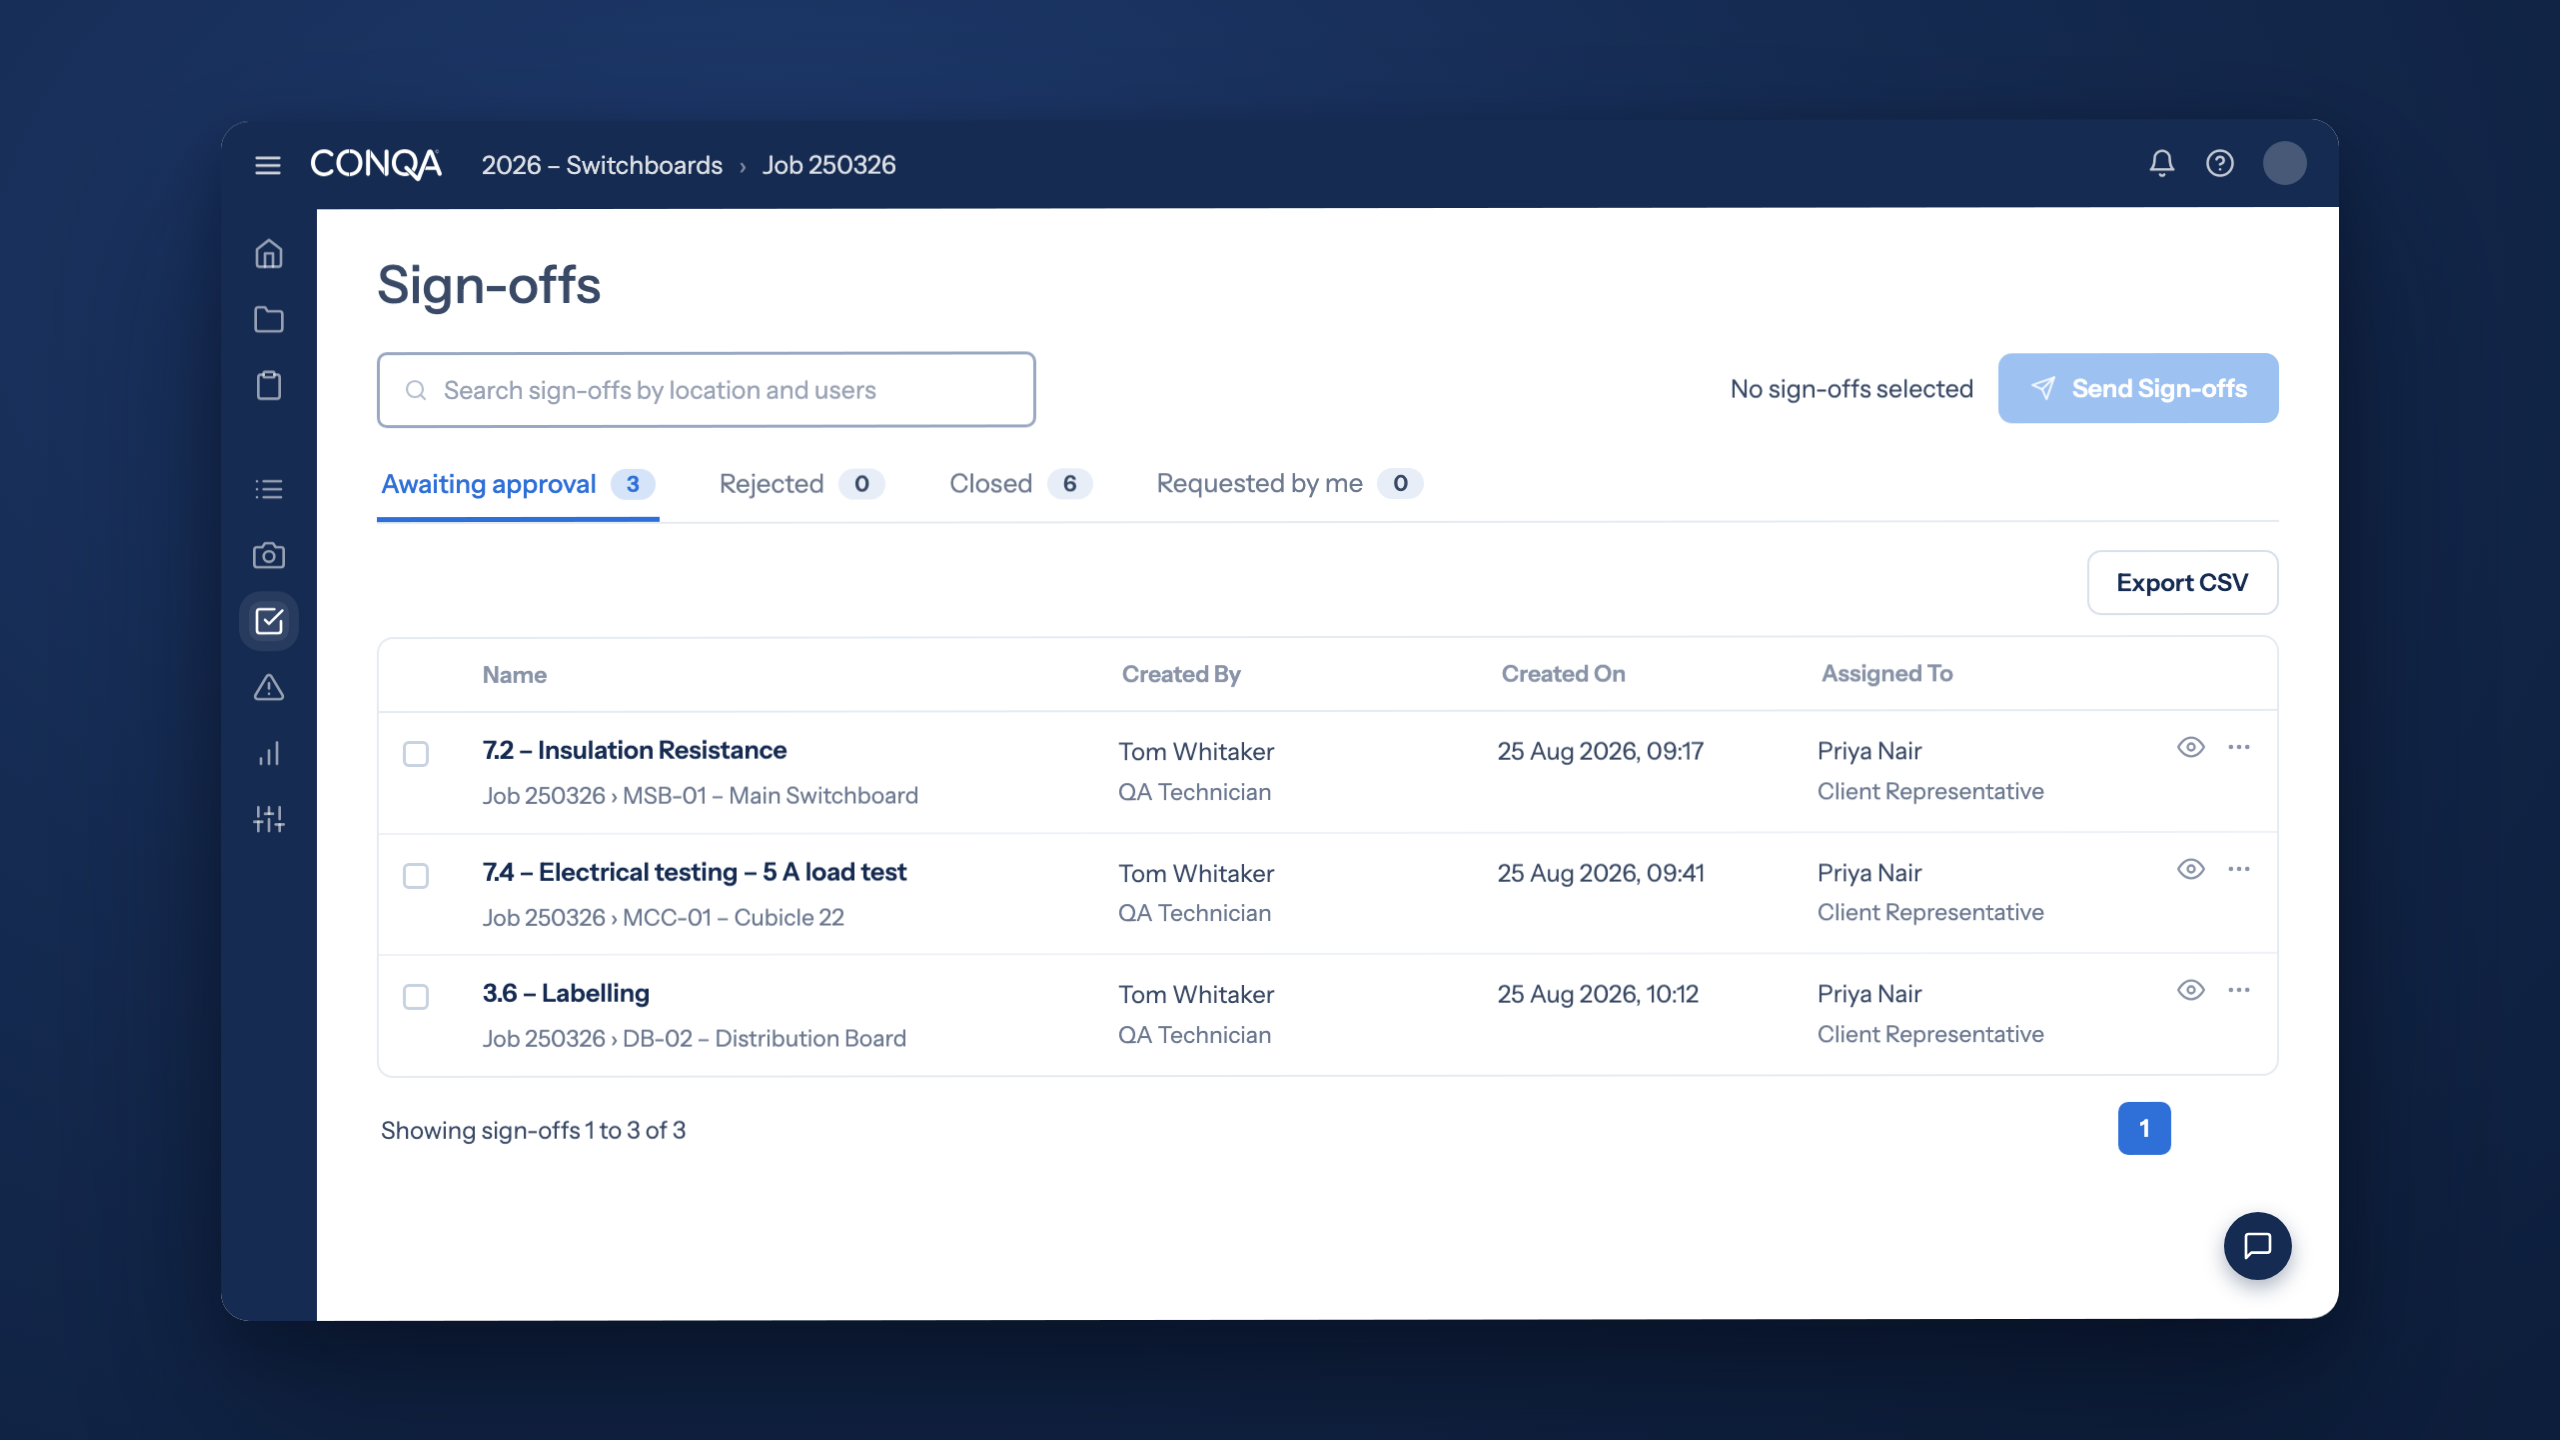
The record behind the test, ready to show the day the client walks the floor.
What switchboard manufacturers told us.
We manufacture a repeat client’s meter panels – 60-odd over two years. In CONQA we have every record: the evidence of the very first one, down to where the labels sit.
– a switchboard manufacturer“One good catch with a good system could save us a huge amount of money.”
– a QA lead at a switchboard manufacturer“I can’t see why they would change.”
– a switchboard manufacturerCommon questions
What does CONQA do for switchboard manufacturers?
CONQA is construction quality assurance software built on proof. Tests and sign-offs are captured as the board is built and filed against the unit itself, so every board leaves the factory with a permanent record of what was built, what was tested, who signed it off and what it looked like at dispatch. That record answers for the board if it is ever questioned.
Can CONQA help with a disputed board after dispatch?
That is the job it is built for. The record shows the state the board left the factory in – test results, sign-offs and photos, dated before dispatch. One switchboard manufacturer rebutted a megger-test dispute straight from the record, from a phone, and answered a damaged-in-transit cable claim the same way. Without the record, the cost of a disputed board defaults to the maker.
How does CONQA support factory acceptance testing?
The record behind the FAT is built as the board moves through the shop, so there is nothing to assemble when the client arrives. They walk the board with a printed or emailed report showing every check signed and every test result filed against the unit – readings and photos, not pages of ticks. The same record carries the handover pack and the next tender.
Can CONQA handle complex boards like MCCs?
Yes. Each cubicle on a motor control centre carries its own checklist and test record – on a thirty-cubicle MCC that is thirty individual records. When one motor is questioned, you produce that cubicle’s tests, photos and sign-offs, not a single report for the whole board.
Does CONQA replace our ERP or production systems?
No. CONQA is the independent QA record. It runs alongside your ERP, scheduling system and spreadsheets rather than replacing them. The record is exportable in full and yours to keep. It outlives the project and the person who made it.
What does implementing CONQA involve?
Less than the word suggests. There is no migration – the record starts on the next board, not with the backlog – and no integration: boards are added one at a time as they reach QA, which is how the switchboard manufacturers we work with choose to run it. A generic board checklist works from day one, and your own team adds board-specific templates as they need them. One manufacturer went from fully paper with a QA manager a few weeks into the job; twelve months later his verdict was “I can’t see why they would change.”
We’re flat out – is now the right time?
Flat out is the case for starting, not against it. A rush week is exactly when paper falls behind – one manufacturer described boards shipping three weeks ahead of their paperwork – and every board that leaves without a record is unprotected for the length of its liability window. Starting doesn’t interrupt production: the next board gets checked in CONQA instead of on paper, and the ones after it follow. Nothing stops, and nothing has to catch up.
How much does CONQA cost?
CONQA starts at $899 a month for manufacturers. Pricing scales with the size of your operation – there’s no per-user charge, so everyone who needs to see the record gets access. Book a demo and we’ll give you a firm number for your workshop.
No migration. No integration. The record starts on the next board that reaches QA – a generic board checklist from day one, your own templates as you need them. Nothing to move, nothing to catch up.
The board leaves. The proof leaves with it.
See the record a board carries out of the workshop.